28 October 2026 | Wednesday | News
Made Scientific to integrate multiple UniFuge® single-use centrifugation systems across its Princeton, NJ, and East Norriton, PA, facilities to support its 3D bioreactor platforms, with CARR naming Made Scientific a preferred CDMO for UniFuge development studies
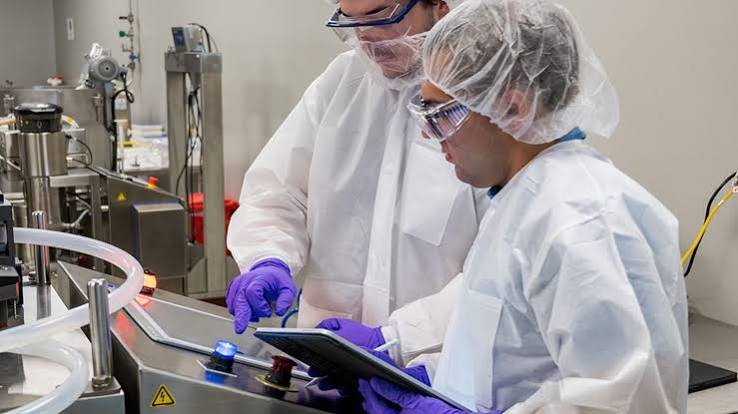
Made Scientific, Inc., a leading U.S.-based clinical- and commercial-stage cell therapy contract development and manufacturing organization (CDMO), and CARR Biosystems, an innovator in cell processing and centrifugal separation technologies for bioprocessing, today announced a partnership under which Made Scientific will deploy multiple CARR UniFuge® single-use centrifugation systems across its Princeton, NJ, and East Norriton, PA, facilities. Made Scientific will integrate UniFuge into its operations as a robust cell harvest, wash, and concentration technology for 3D and large-scale manufacturing of mesenchymal stem cells (MSCs) and feeder cells, strengthening its ability to support allogeneic programs as they scale.
"Allogeneic therapies reach patients at commercial scale only when the whole process scales, not just the bioreactor," said Syed T. Husain, Chairman and CEO of Made Scientific. "As we bring 3D bioreactor capacity online, harvest and wash is where large-volume processes are most often constrained or where significant yields are lost. Integrating CARR's UniFuge platform across our Princeton and East Norriton network gives our clients a robust, closed, and automated processing option from development through commercial supply."
The UniFuge platform uses low-shear tubular bowl centrifugation to support cell concentration, washing, media exchange, harvest, and formulation. It maintains high cell viability and product recovery. Its single-use family spans process volumes from milliliters to more than 2,000 liters, and it offers automated operation, rapid changeover, and a 21 CFR Part 11–compliant data trail. Together, these features help manufacturers carry a consistent separation step from process development into GMP production.
Made Scientific is equipping its East Norriton facility with scalable 3D bioreactor platforms of up to 200 liters, and UniFuge will provide a closed, automated separation step for its MSC and feeder cell processes as those programs scale.
Made Scientific will integrate the UniFuge systems into its existing development and GMP manufacturing workflows, complementing the broad portfolio of closed and automated technologies the company already operates. For sponsors, the partnership creates a more direct path from early-phase manufacturing to commercial readiness. Process development work at smaller scale can translate to larger volumes on the same technology, which supports comparability, reduces scale-up risk, and helps programs advance efficiently as demand grows.
The companies also plan joint development studies, using CARR's benchtop UFMini® system to generate small-scale data that carries forward to larger volumes, and Made Scientific will serve as a preferred CDMO for CARR customers evaluating the platform.
Made Scientific's MSC and extracellular vesicle (EV) offerings were established through its partnership with RoosterBio, which has developed scalable 2D flask and 3D bioreactor manufacturing platforms for MSCs and EVs. RoosterBio has also recently integrated the UniFuge platform into its bioprocess engineering capabilities and process development services. As sponsor programs leveraging RoosterBio's MSC and EV bioprocesses featuring UniFuge transition into Made Scientific's GMP operations, sponsors will benefit from seamless technology transfer from development to GMP manufacturing.
"Made Scientific's expanding clinical-to-commercial footprint make it an ideal partner for scalable, single-use cell processing," said Joel Williams, President of CARR Biosystems. "Their team's manufacturing expertise and focus on scale-up align closely with how we designed the UniFuge platform. Together, we can help cell therapy developers bring processes from the clinic to commercial supply with confidence."
With the recent acquisition of its operational GMP facility in East Norriton and its established operations in Princeton, Made Scientific continues to strengthen the technologies and infrastructure that support cell therapy programs at every stage of development. Its partnership with CARR Biosystems further positions the company to meet growing demand for commercial-ready cell therapy manufacturing.


© 2026 Biopharma Boardroom. All Rights Reserved.